Automatic Mini Rice & Coffee Bean Color Sorter Small CCD Separator Machine for Grading & Sorting
- PRODUCT DETAIL
1 Overview of the Color Sorter Machine
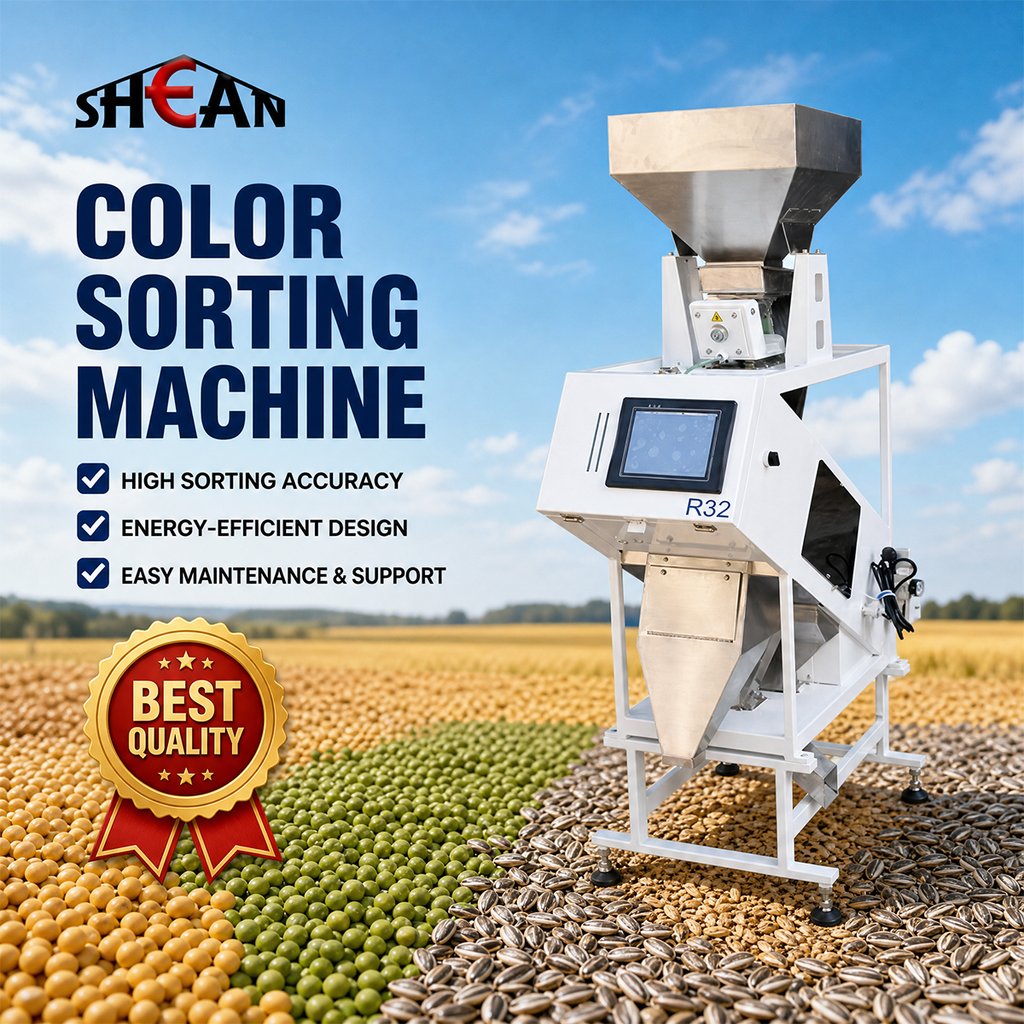
An automatic color sorter machine is an advanced optical sorting solution designed to identify and separate materials according to their color differences and other detectable visual characteristics. By combining high resolution imaging technology intelligent image processing and a precision rejection system the machine helps manufacturers improve product quality reduce impurities and achieve more consistent sorting results
Our color sorting machine is suitable for a wide range of agricultural products food processing materials and industrial applications. It can help processing plants separate discolored particles foreign materials and defective products from acceptable materials according to the selected sorting criteria
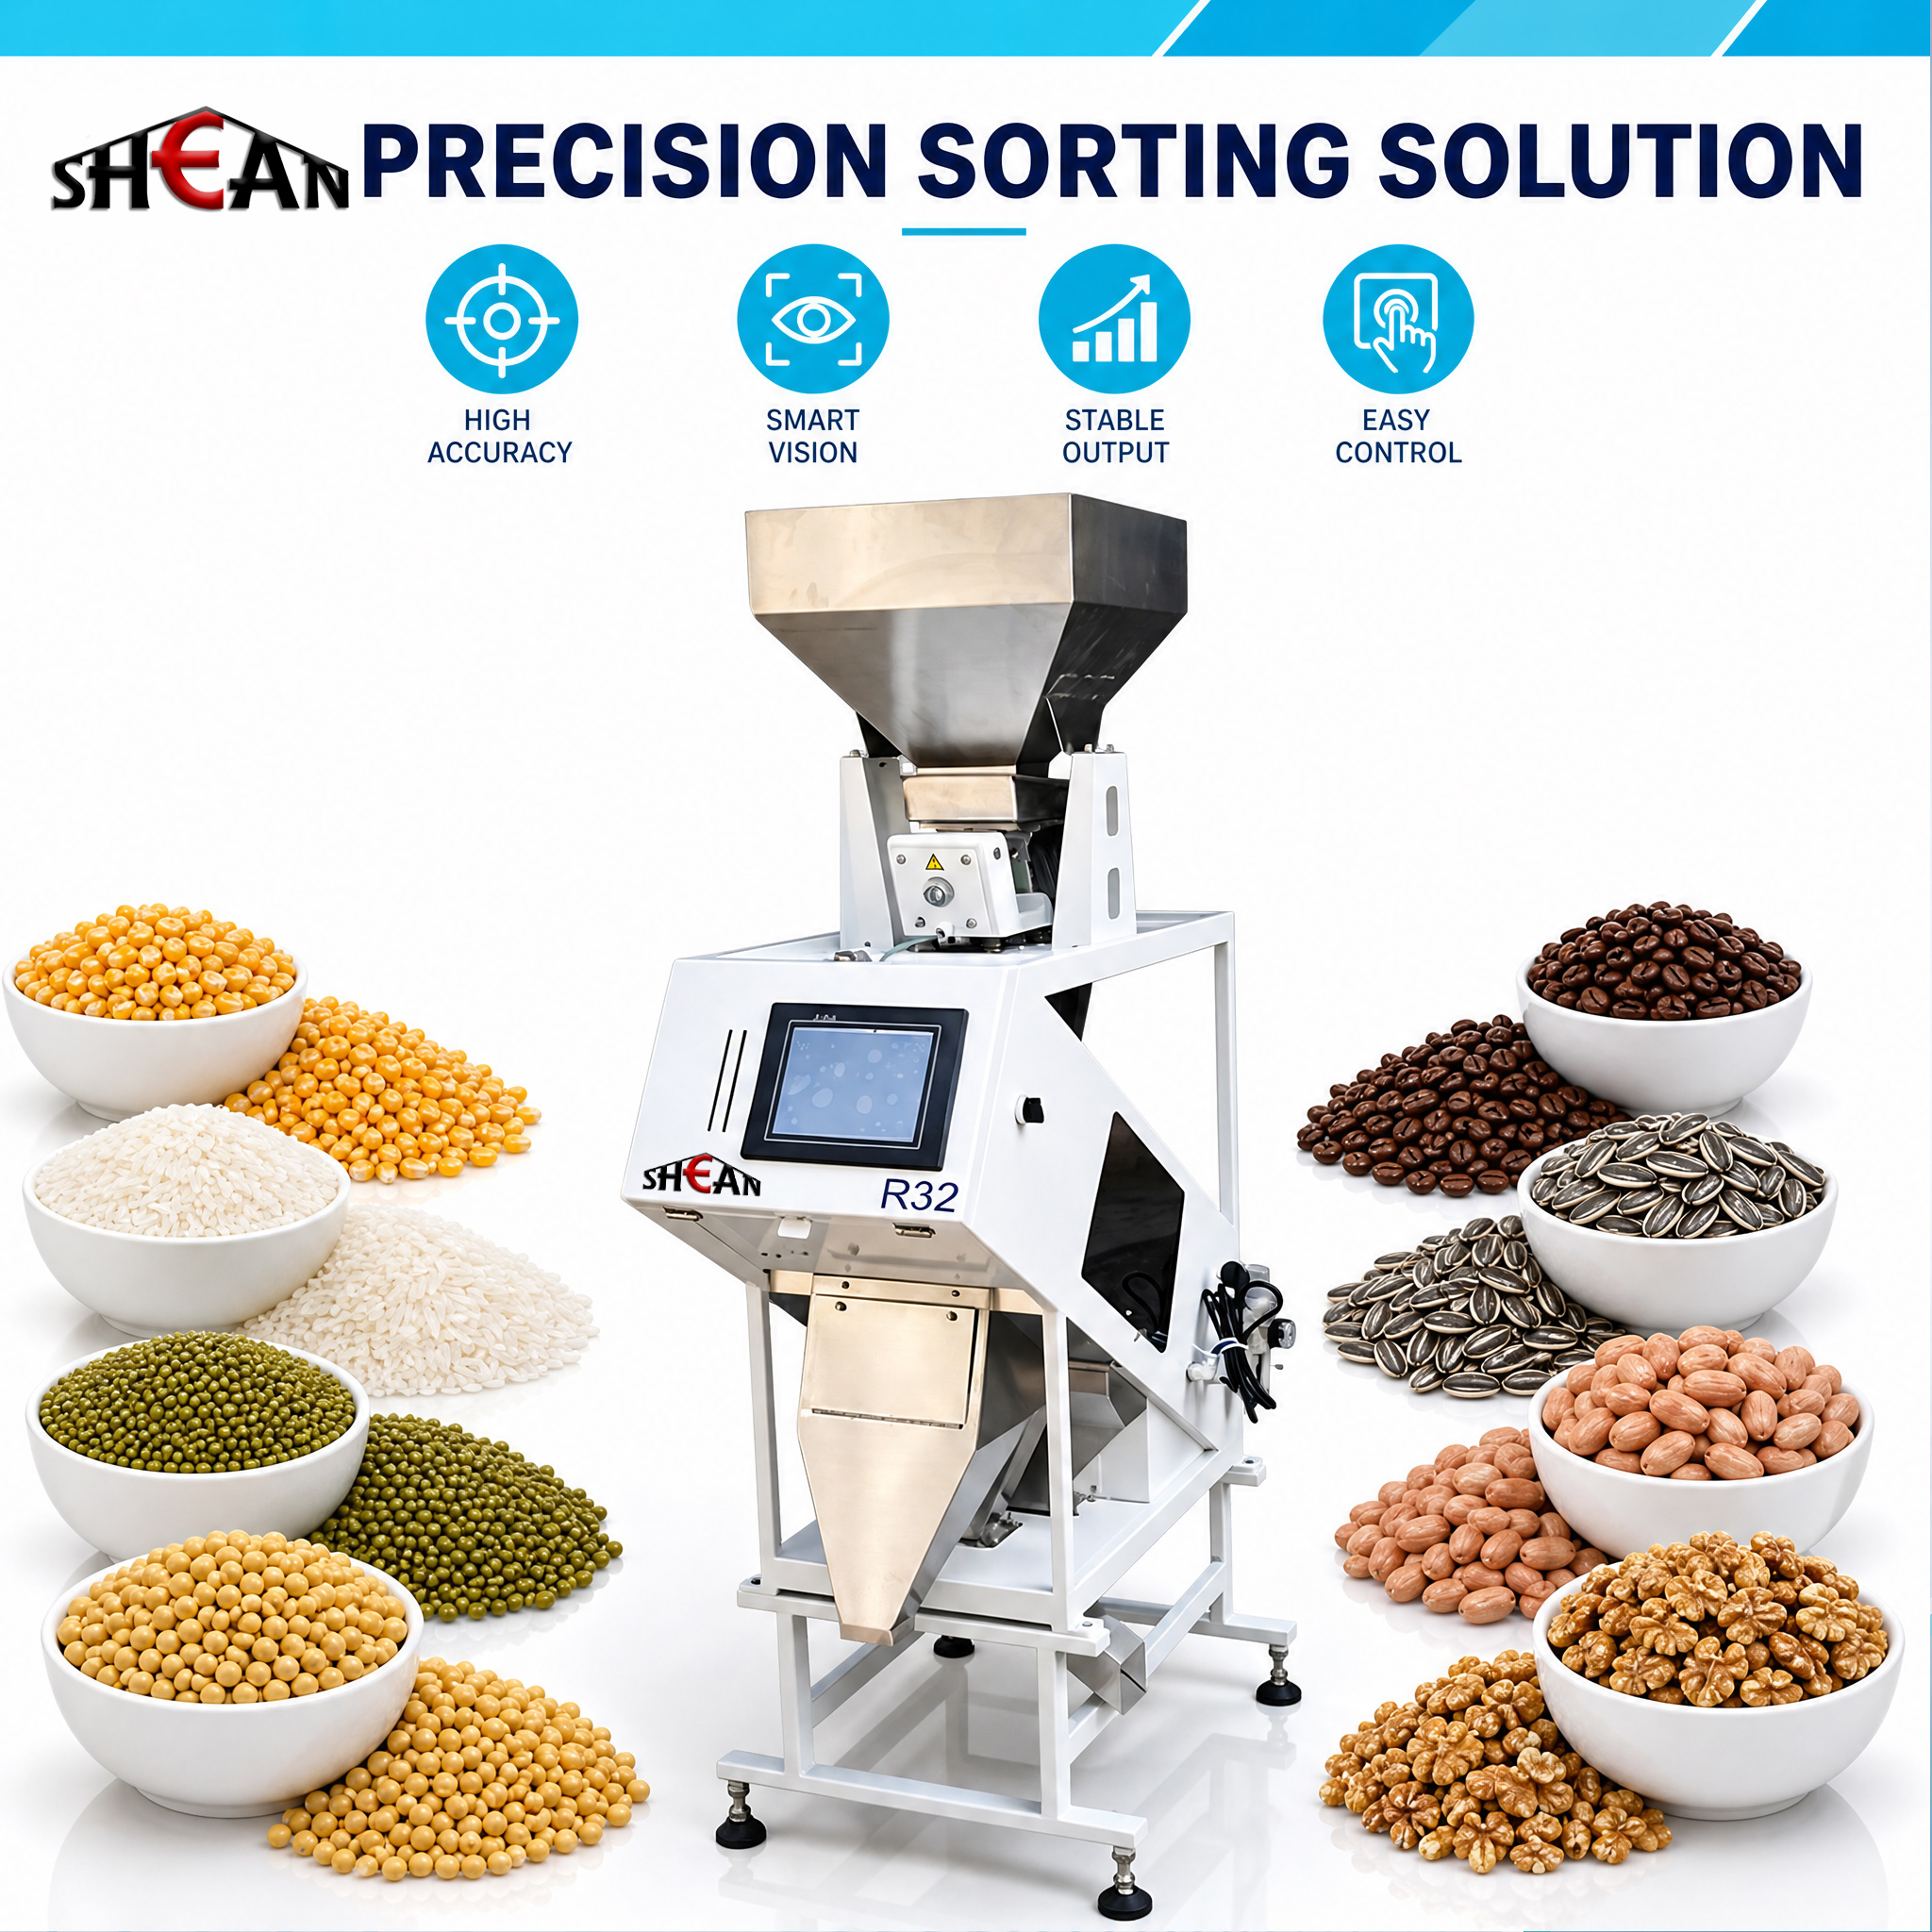
Whether you process rice grains beans seeds nuts or other suitable granular materials a reliable optical color sorter can improve production efficiency and support consistent product quality
2 Key Advantages of Our Color Sorter Machine
High Precision Optical Recognition
The optical recognition system captures images of materials passing through the sorting area and analyzes detectable differences between target products and unwanted particles. Depending on the machine configuration the system can identify color variations stains discoloration and selected visible defects
Accurate recognition helps improve sorting consistency and reduce the amount of unwanted material in the finished product
Intelligent Image Processing System
The intelligent control system processes image information and applies configured sorting parameters to distinguish acceptable materials from rejected particles. Operators can adjust relevant settings according to the raw material characteristics and sorting requirements
This makes the color sorter suitable for different product grades and changing production conditions
High Speed Sorting Performance
Designed for continuous material processing the machine coordinates material feeding optical detection and rejection operations in an integrated workflow. Appropriate configuration helps processing facilities improve throughput and reduce dependence on manual inspection
Actual sorting capacity depends on the material type moisture content impurity level required sorting accuracy and selected machine model
Precision Air Jet Rejection System
When the system detects an unwanted particle the rejection mechanism activates the corresponding air jet to remove it from the acceptable material stream. Fast and targeted rejection helps separate defective particles while minimizing the loss of qualified products
The rejection system should be configured according to the characteristics of the material and the required sorting performance
User Friendly Control Interface
The intelligent control interface allows operators to manage sorting parameters monitor equipment operation and select appropriate product settings. A clear interface helps simplify daily operation and supports convenient adjustment when changing between compatible materials
Stable Structure and Convenient Maintenance
A well designed machine structure supports continuous operation in commercial processing environments. Accessible components and routine cleaning procedures help maintain stable performance and reduce unnecessary downtime
3 How Does a Color Sorter Machine Work
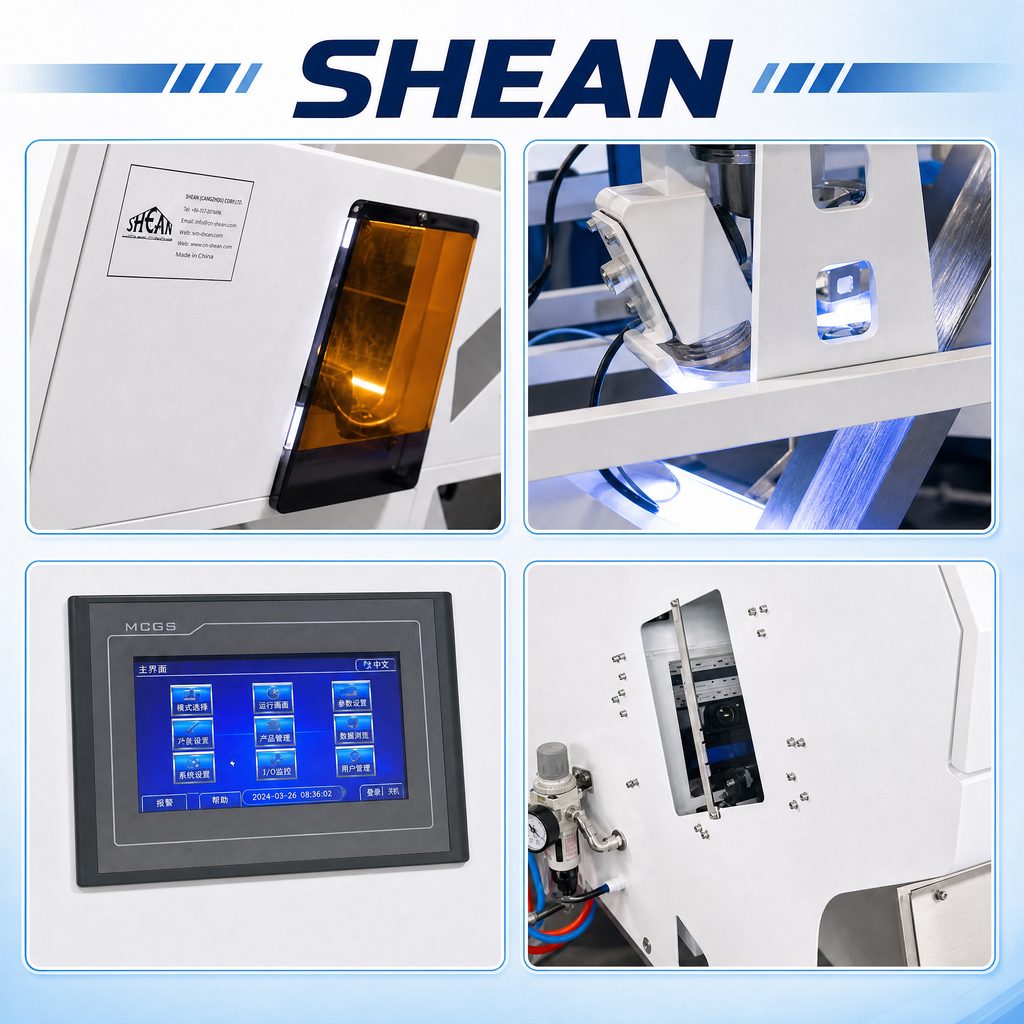
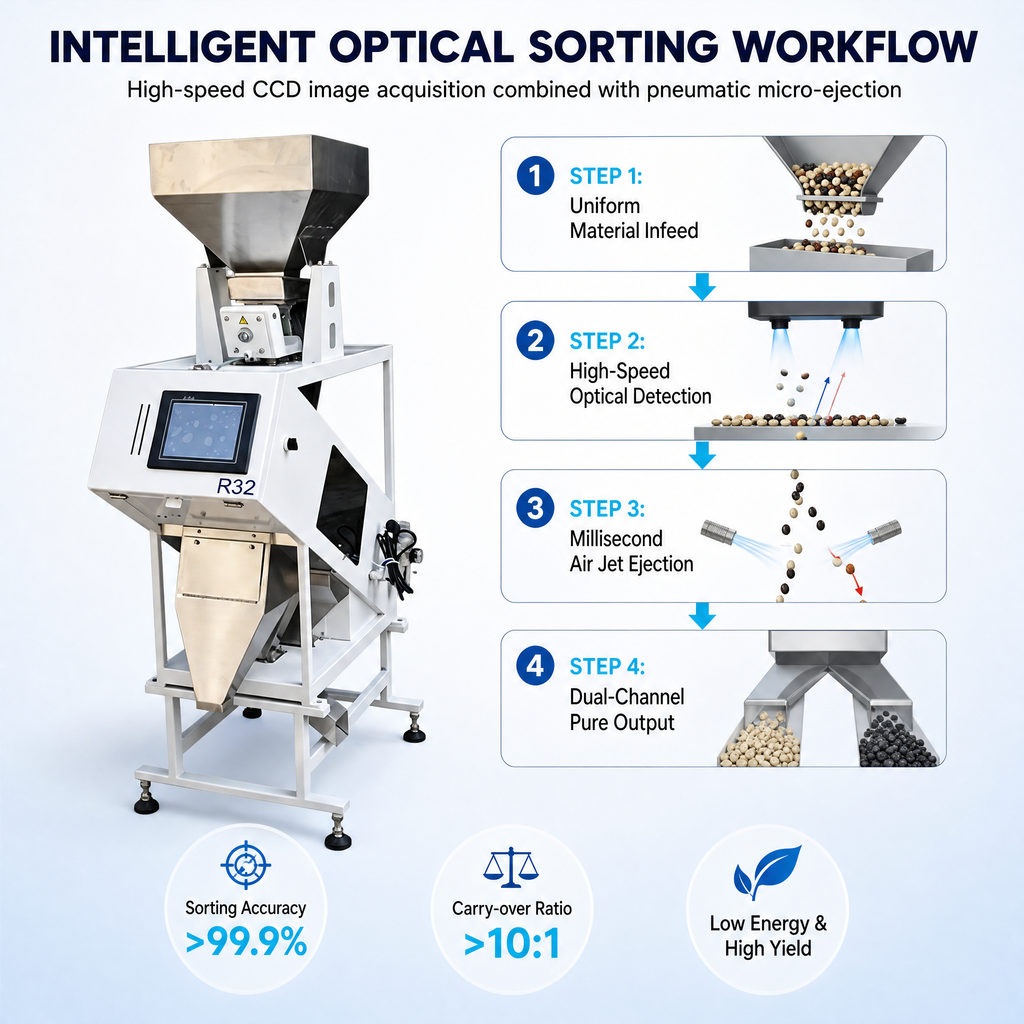
The color sorting process generally includes the following stages
Step 1 Material Feeding
Raw materials enter the feeding system and are distributed into a controlled flow to help maintain stable material presentation during sorting
Step 2 Optical Detection
Materials pass through the optical detection area where cameras and lighting systems capture relevant visual information. The optical system identifies differences according to the machine configuration and selected sorting criteria
Step 3 Intelligent Analysis
The image processing system analyzes the collected information and determines which particles meet the rejection criteria
Step 4 Automatic Rejection
The rejection system removes selected defective particles or unwanted materials from the product stream using precisely controlled air jets
Step 5 Finished Material Collection
Acceptable materials and rejected particles are directed into separate collection outlets for further processing inspection or packaging
The complete process helps automate material inspection and improve sorting consistency in suitable production environments
4 Wide Applications of the Color Sorting Machine
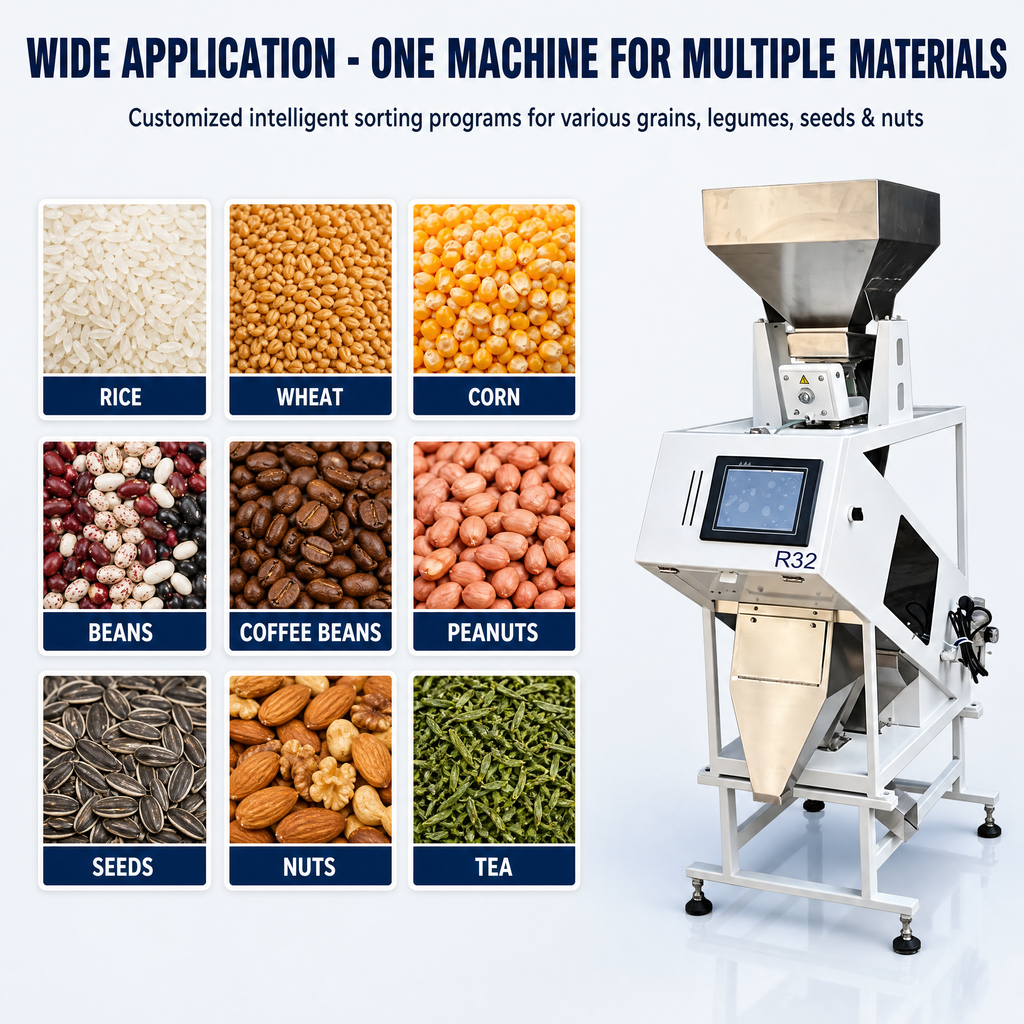
Rice and Grain Processing
A rice color sorter can help remove discolored rice broken or visually defective grains and selected unwanted particles depending on the sorting configuration. It is suitable for rice mills grain processing plants and agricultural product exporters
Beans and Pulses
The machine can sort suitable beans peas lentils and other pulses according to visible color differences and selected defect characteristics. It helps processors improve the appearance and consistency of finished products
Seeds and Agricultural Products
Seed processors can use optical sorting equipment to separate visibly different particles and unwanted materials where the detection system is suitable for the target product
Nuts and Dried Food Products
Compatible sorting configurations can be used for selected nuts dried fruits and other granular food products to identify visible defects and color variations
Industrial Materials
Depending on the optical system and material characteristics color sorting technology can also be applied to selected plastics minerals and other industrial particles
Material testing is recommended before purchase to confirm detection capability sorting accuracy processing capacity and expected product recovery
5 R32 Color Sorter Machine for Commercial Processing
For businesses considering an R32 color sorter machine the appropriate configuration should be selected according to the target material production requirements and sorting objectives
Before choosing an R32 model buyers should confirm the number of sorting channels the optical system configuration the required processing capacity the available installation space and the expected impurity removal performance
A properly configured color sorting solution can help processing businesses improve product consistency optimize labor allocation and increase the value of sorted materials
Please contact our team for the actual R32 model specifications available options and application recommendations
6 Benefits for Food Processing Plants and Distributors
Investing in an automatic color sorter machine can provide several operational benefits
Improved Product Quality
Automated optical inspection helps identify selected visible defects and unwanted particles more consistently than manual sorting alone
Higher Processing Efficiency
Continuous automatic sorting supports larger processing volumes and reduces reliance on labor intensive inspection
Reduced Material Waste
Appropriate detection and rejection settings help balance impurity removal with the recovery of qualified products
Consistent Product Appearance
More uniform color and fewer visible defects can help businesses meet customer requirements and maintain product standards
Flexible Production Applications
Suitable machine configurations can support different materials and sorting specifications helping businesses adapt to changing market demand
7 How to Choose the Right Optical Color Sorter
Selecting the right color sorter requires more than comparing machine prices. Buyers should evaluate the following factors
Raw Material Type and Characteristics
Identify the material size shape color range moisture level and typical defects that need to be removed
Required Processing Capacity
Determine the expected hourly throughput and the production requirements of the existing processing line
Sorting Accuracy and Product Recovery
Clarify the acceptable impurity level and the desired recovery rate for qualified materials
Optical and Software Configuration
Confirm whether the available camera lighting and image processing systems can detect the specific defects in your material
Installation and After Sales Support
Consider available factory space electrical requirements air supply maintenance access operator training and technical support
Providing representative material samples and clear sorting objectives helps suppliers recommend a more suitable configuration
8 Why Work With Us
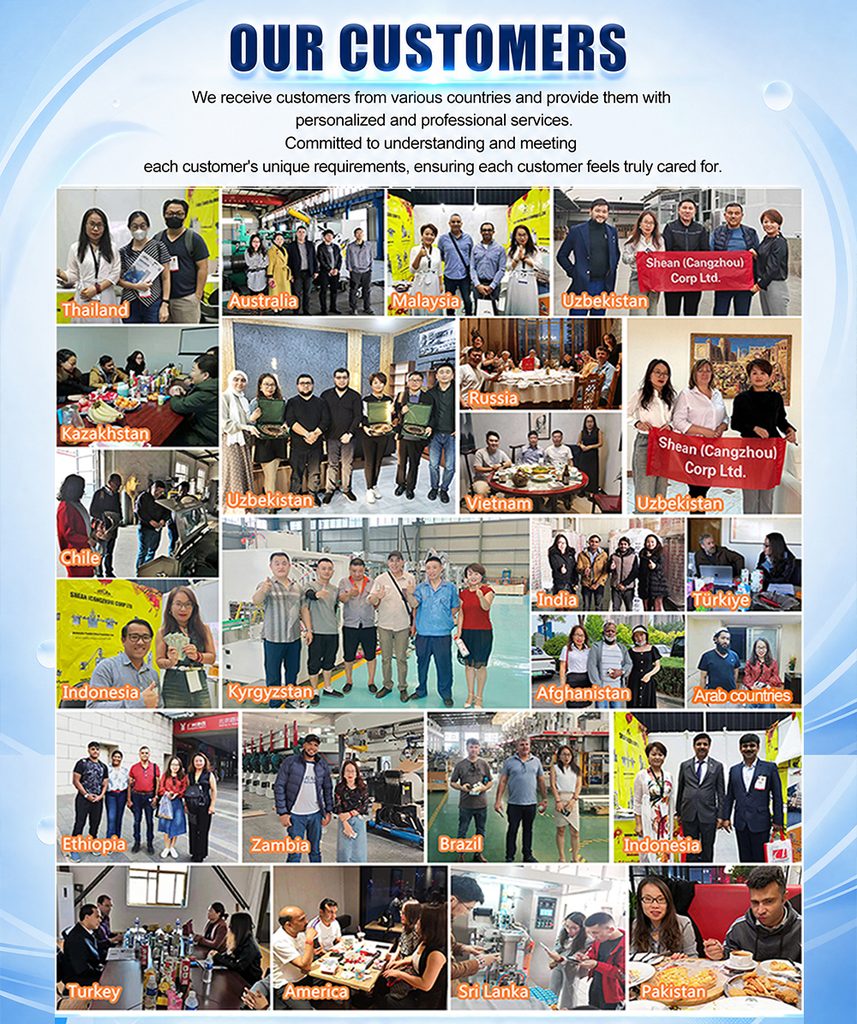
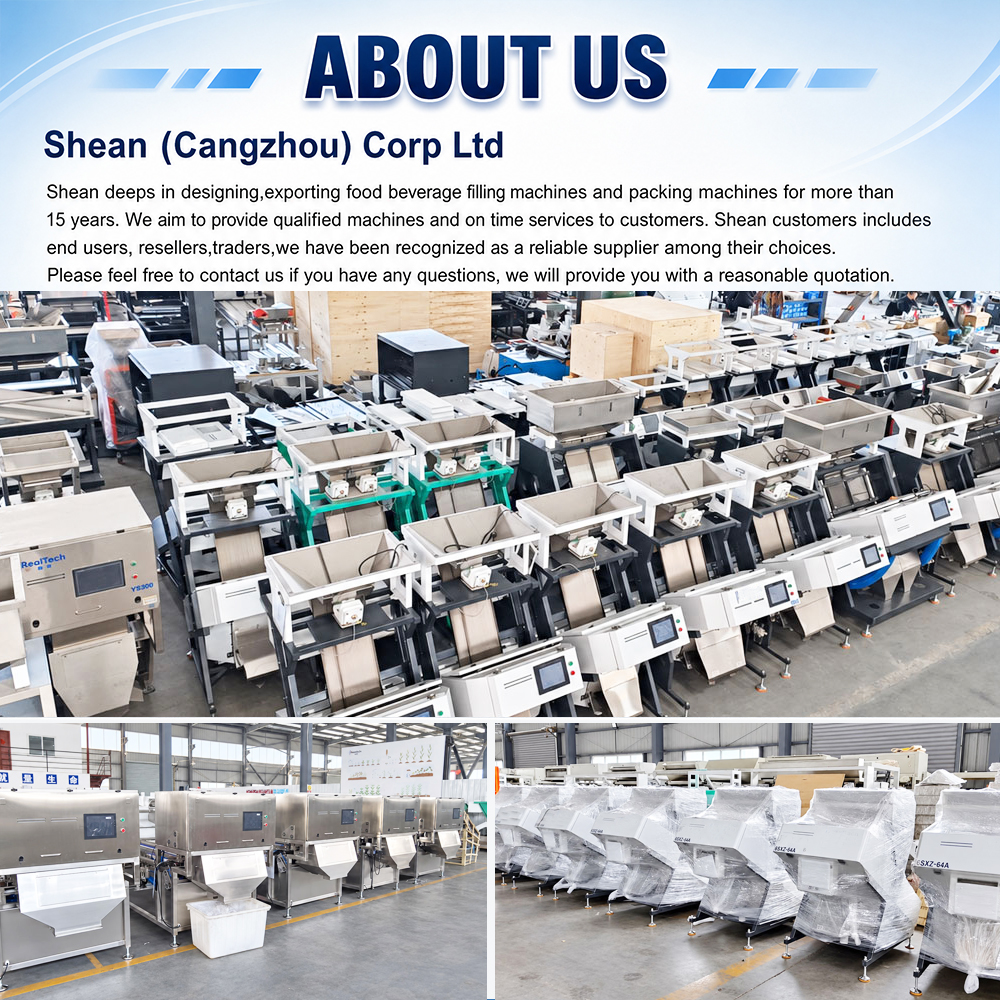
We provide color sorting equipment solutions for businesses seeking to improve material quality and automate sorting operations. Our team can help evaluate your application requirements and identify suitable equipment configurations based on the material type production capacity and sorting objectives
For overseas buyers we can discuss technical specifications customization requirements installation planning spare parts and international shipping arrangements according to the project scope
Our goal is to help customers select practical optical sorting equipment that supports stable production and long term business development
9 Request a Quote for Your Color Sorter Machine
Looking for a reliable automatic color sorter machine for your processing facility
Contact us with the following information
Your raw material type and product photos
Expected processing capacity per hour
The main impurities or defects you need to remove
Your required sorting accuracy and finished product quality
Your factory location and production line requirements
Our team can evaluate your application and recommend a suitable color sorting solution for your business
Contact us today to learn more about our color sorter machines technical specifications and available sorting options
- RELATED PRODUCTS


